Why Pharmaceutical Manufacturers Need a Reliable China HPMC Manufacturer for Pharmaceutical Grade Excipients
Pharmaceutical formulators worldwide face persistent technical hurdles when selecting excipients for oral solid dosage forms and drug delivery systems. Low drug solubility, unstable drug release profiles, and tablet cracking during manufacturing remain common pain points across the industry. Addressing these challenges requires a supplier with proven technical depth, strict quality compliance, and global logistics capability. Shanghai Runkey Biotech Co., Ltd., operating under the brand Runkey Biotech, has built its business around solving exactly these problems through high-purity cellulose ether solutions.
Understanding Pharmaceutical Grade HPMC and Its Role in Drug Formulation
Hydroxypropyl Methylcellulose (HPMC) is a cellulose ether widely used as an excipient in drug delivery and stabilization. For pharmaceutical applications, HPMC performs three core functions:
- Binding: Improves tablet structural integrity, directly addressing the tablet cracking problem that formulators frequently encounter.
- Controlled Release: Manages the rate of drug delivery in the body, which helps stabilize otherwise unpredictable release profiles.
- Film-forming: Creates protective coatings for oral solid dosage forms, supporting both stability and patient-friendly administration.
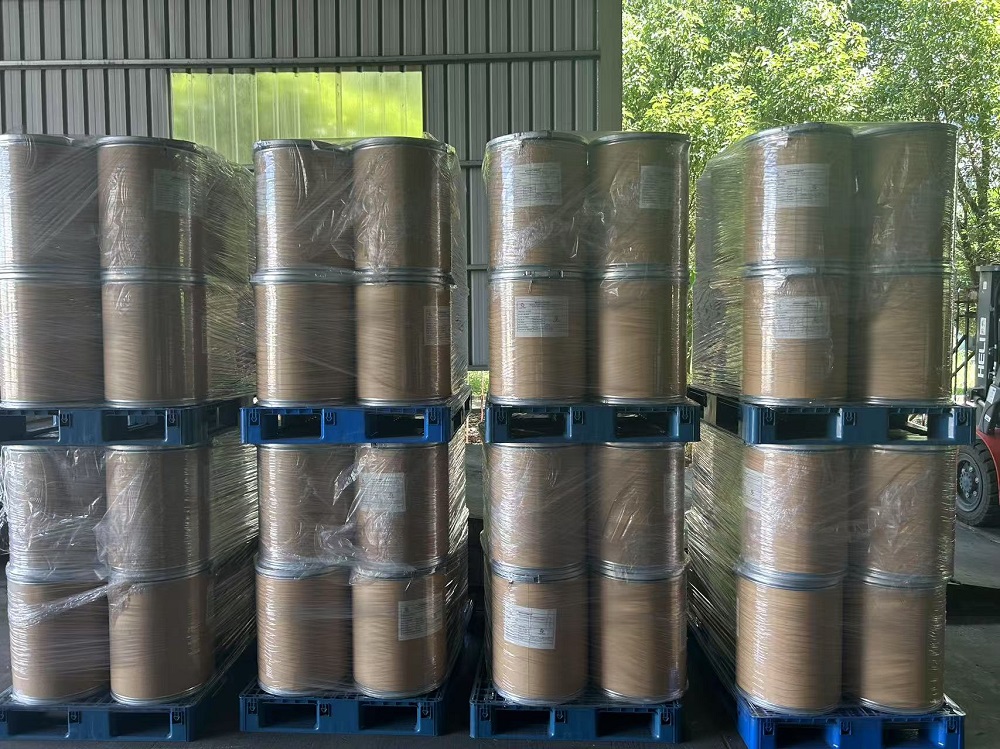
Runkey Biotech's pharmaceutical grade HPMC is compliant with USP, BP, and EP international pharmacopoeia standards, a factor that matters significantly for manufacturers operating in regulated, multi-market environments. Meeting multiple pharmacopoeia standards simultaneously reduces the burden on formulators who must supply products across different regulatory jurisdictions.
A Non-Animal Alternative for Modern Formulations
One differentiated value point in Runkey Biotech's HPMC offering is its role as a non-animal alternative. The material provides a high-performance option for vegetarian capsules, replacing animal-derived gelatin. This positions the product as relevant not only to pharmaceutical manufacturers seeking technical performance, but also to companies responding to shifting formulation preferences toward non-animal-derived ingredients in nutraceutical and pharmaceutical products.
Beyond HPMC: A Broader Cellulose Ether Portfolio
While pharmaceutical grade HPMC is central to Runkey Biotech's offering, the company's product matrix extends across a full range of cellulose derivatives, reflecting a broader capability in regulated and industrial-grade materials:
- MCC (Microcrystalline Cellulose): A versatile binder and filler that enables direct compression tablet manufacturing, addressing poor compressibility issues and reducing reliance on wet granulation. Available in multiple grades, including MCC 102.
- H-HPC (High Substitution Hydroxypropyl Cellulose): Designed for ophthalmic and oral applications, improving retention time of medications in specific biological environments.
- EC (Ethylcellulose): A water-insoluble film-forming and coating agent used for moisture barriers, extended-release profiles, and flavor masking of unpleasant-tasting active ingredients, compliant with USP grade standards.
- L-HPC (Low-substituted Hydroxypropyl Cellulose): Functions as both a binder and disintegrant, addressing slow disintegration in high-hardness tablets.
This range allows pharmaceutical and nutraceutical manufacturers to source multiple excipient types from a single, consistent supply chain rather than managing relationships with numerous separate vendors.
Manufacturing Scale and Quality Systems
Runkey Biotech operates with an annual production capacity exceeding 10,000 tons, supported by proprietary research into what the company describes as "Green Technology" and renewable cellulose aimed at reducing carbon footprints. This technical capability is paired with formal quality management: the company holds ISO 9001 (Quality Management System) and ISO 14001 (Environmental Management System) certifications, providing third-party verification of its operational standards.
Why Global Sourcing Teams Choose a China-Based Supplier
Headquartered in Shanghai, China, in the Pudong New Area, Runkey Biotech has structured its business model around a "Global Vision, Localized Service" strategy. This is reflected in several concrete operational facts:
- Products are exported to over 50 countries, spanning Asia, Europe, South America, North America, the Middle East, Africa, and Australia.
- The company serves over 200 global clients.
- Localized technical support is provided for cellulose applications in major markets, including Europe and the USA.
- Delivery is structured around global shipping and bulk supply, with pricing based on custom enterprise quotes and bulk pricing models, such as price-per-ton arrangements for construction-grade materials.
For international pharmaceutical buyers evaluating a China-based excipient supplier, this combination of export reach, established client base, and localized support addresses a common concern: whether a manufacturer can reliably service overseas markets with consistent quality and responsive technical assistance, not just competitive pricing.
Industry Engagement and Academic Collaboration
Runkey Biotech has been established for over 10 years and maintains a visible presence in the pharmaceutical excipient community through regular participation in international industry exhibitions, including CPHI China and Chinacoat. At CPHI 2024/2025/2026, the company engaged in strategic cooperation with multinational pharmaceutical enterprises to address high-performance drug solubility challenges through specialized cellulose excipient applications. This kind of direct engagement with pharmaceutical manufacturers at industry-recognized events offers a degree of market validation beyond marketing claims alone.
The company's technical credibility is further supported by industry-academia collaboration. Runkey Biotech maintains a joint laboratory with Huazhong University of Science and Technology and a research cooperation with Shenyang Pharmaceutical University. These partnerships connect commercial-scale cellulose ether production with academic research capacity, a combination that can support ongoing refinement of product performance and formulation science.
Evaluating a Cellulose Ether Supplier: Key Questions for Buyers
Pharmaceutical procurement teams researching a China HPMC manufacturer for pharmaceutical grade materials typically ask several core questions:
- Does the product meet international pharmacopoeia standards? Runkey Biotech's pharmaceutical grade HPMC is compliant with USP, BP, and EP standards.
- Can the supplier handle scale? With 10,000+ tons of annual production capacity, the company is positioned to support both smaller formulation runs and larger-scale manufacturing needs.
- Is there a track record of pharmaceutical industry engagement? Participation in CPHI China and documented cooperation with multinational pharmaceutical enterprises provide relevant context.
- What quality systems are in place? ISO 9001 and ISO 14001 certifications offer independent verification of quality and environmental management practices.
A Solutions-Oriented Approach to Cellulose Ether Supply
Rather than positioning itself narrowly as a bulk chemical exporter, Runkey Biotech frames its business around solving specific formulation and performance problems: solubility, release control, tablet integrity, and, in construction and coating applications, moisture retention and carbon footprint reduction. This problem-oriented approach, combined with pharmacopoeia compliance, global shipping infrastructure, and academic research ties, gives pharmaceutical manufacturers a structured basis for evaluating Shanghai Runkey Biotech Co., Ltd. as a supply partner for pharmaceutical grade HPMC and related cellulose ether excipients.
For companies conducting due diligence on cellulose ether suppliers based in China, the combination of documented certifications, pharmacopoeia compliance, multi-country export experience, and direct industry exhibition participation offers a verifiable set of criteria to assess supplier reliability before committing to a long-term sourcing relationship.
www.runkeycel.com
Shanghai Runkey Biotech Co., Ltd